Content Menu
● 1. Ningbo Everheal Medical Equipment Co., LTD.
● 2. Shanghai Joygoal Food Machinery Co., Ltd.
● 3. Guangzhou Mingyue Packaging Machinery Co., Ltd.
● 4. Wenzhou Chunlai Packing Machinery Co., Ltd.
● 5. Jiangsu ASG Packaging Machinery Group Co., Ltd.
● 6. Shenzhen Penglai Industrial Corporation Limited
● 7. Zhangjiagang King Machine Co., Ltd.
● 8. Shantou Today Machine Co., Ltd.
● 9. Ruian Huadong Packing Machinery Co., Ltd.
● 10. Hangzhou Zhongya Machinery Co., Ltd.
● How to Choose the Right Liquid Packing Machine Manufacturer
● Market Outlook for Liquid Packing Machine Manufacturers in China
● Conclusion
● FAQ
>> 1. What industries use liquid packing machines?
>> 2. What is the difference between automatic and semi‑automatic liquid packing machines?
>> 3. How can I ensure a liquid packing machine meets GMP or FDA standards?
>> 4. What maintenance do liquid packing machines require?
>> 5. Can these machines handle different viscosity levels?
China has become a global hub for advanced manufacturing technologies, and among them, Liquid Packing Machine Manufacturers play a crucial role in supplying high‑performance solutions to industries ranging from pharmaceuticals to food and cosmetics. These manufacturers combine innovation, automation, and reliability to meet strict international standards and growing production needs.
In this article, we highlight the top 10 liquid packing machine manufacturers in China renowned for their engineering excellence, customization capabilities, and after‑sales service. Whether you're a producer seeking efficient filling and sealing equipment or a company planning a full factory layout, these enterprises represent the best China has to offer.
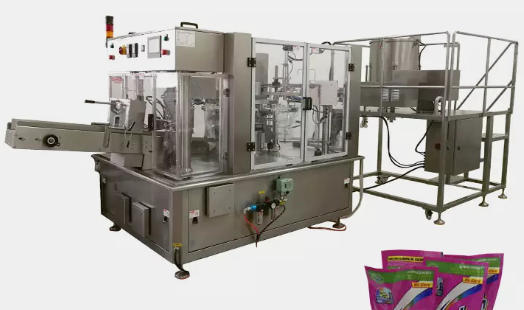
1. Ningbo Everheal Medical Equipment Co., LTD.
Ningbo Everheal Medical Equipment Co., LTD. stands out as a leading name among China's Liquid Packing Machine Manufacturers, specializing in pharmaceutical processing and packaging solutions. With decades of experience and a dedicated R&D team, Everheal provides integrated production line services, including pure water preparation systems, pure steam generators, multi‑effect distillation systems, liquid filling and sealing machines, and sterilization equipment.
What makes Everheal unique is its comprehensive approach to customized plant design and turnkey solutions. The company's team collaborates closely with clients to develop layouts optimized for cleanroom standards, GMP compliance, and operational efficiency. Each project—from conceptual design to installation and commissioning—is executed under strict quality control.
Everheal machines are built with precision control systems that ensure high filling accuracy, minimal contamination risk, and consistent performance across different viscosity levels. Its liquid filling and sealing machines are widely adopted by hospitals, biotech firms, and pharmaceutical manufacturers around the world.
Key Advantages:
- Complete turnkey factory layout and production line design.
- Compliance with international GMP and FDA standards.
- Advanced automation and PLC control for accurate dosing.
- Outstanding technical support and after‑sales maintenance.
With its focus on innovation and reliability, Ningbo Everheal continues to strengthen its global reputation as a trusted partner for professional liquid packaging production solutions.
2. Shanghai Joygoal Food Machinery Co., Ltd.
Shanghai Joygoal is among the most experienced Liquid Packing Machine Manufacturers serving both food and beverage sectors. The company's product line includes automatic pouch filling machines, bottle filling systems, and liquid sachet packaging lines.
Joygoal stands out for its versatility—their machines can handle juices, dairy products, liquid condiments, and viscous substances like sauces. Combining stainless‑steel construction and ISO‑certified production, their systems ensure hygiene, durability, and efficient throughput.
3. Guangzhou Mingyue Packaging Machinery Co., Ltd.
Guangzhou Mingyue delivers high‑efficiency packaging equipment specialized for pharmaceuticals, cosmetics, and chemicals. Their liquid packing machines are designed for precise filling volumes and adaptive sealing functions. The company focuses on intelligent automation and remote monitoring functions, offering customers complete control over production cycles.
Its consistent emphasis on energy‑saving technologies and user‑friendly designs has earned Mingyue a reputation as a sustainable partner within the Liquid Packing Machine Manufacturers sector.
4. Wenzhou Chunlai Packing Machinery Co., Ltd.
Wenzhou Chunlai is a professional supplier of liquid, paste, and granule packaging solutions, offering a wide range of vertical form‑fill‑seal (VFFS) machines. Their liquid packing machines are built to handle sauce, honey, shampoo, and beverage packaging with high precision.
What differentiates Chunlai is its emphasis on compact machine design and cost‑effective solutions. Ideal for SMEs and startups, the company provides flexible configurations that balance price and productivity.
5. Jiangsu ASG Packaging Machinery Group Co., Ltd.
As one of China's earliest established Liquid Packing Machine Manufacturers, Jiangsu ASG has decades of industry leadership in beverage bottling systems. Their portfolio covers bottle rinsing, filling, and capping equipment, along with PET bottle blowing machines and water treatment plants.
ASG's machines are widely used in large‑scale water, juice, and soft‑drink factories. The group's advanced technology integrates servo motors, electronic flowmeters, and intelligent diagnosis systems, enabling high‑speed, reliable, and low‑waste operation.
6. Shenzhen Penglai Industrial Corporation Limited
Penglai Industrial Corporation is known for producing compact tabletop and fully‑automatic liquid filling machines. Their range of products serves cosmetics, daily chemicals, and pharmaceuticals. The firm has been exporting globally due to its simple, modular machine designs compatible with both semi‑automatic and automatic production lines.
Key advantages include consistent filling accuracy, stainless‑steel construction, and flexible adjustment systems suitable for multiple bottle shapes and sizes.
7. Zhangjiagang King Machine Co., Ltd.
King Machine is an industry leader focusing on complete beverage filling and packaging lines. This manufacturer is recognized globally for full‑turnkey solutions combining water treatment systems, bottle blow molding, filling, and labeling units.
Their liquid filling lines feature integrated sensors for real‑time operation monitoring. Reliable after‑sales service and spare part supply make King Machine a popular choice among international bottling companies seeking comprehensive liquid packaging solutions.
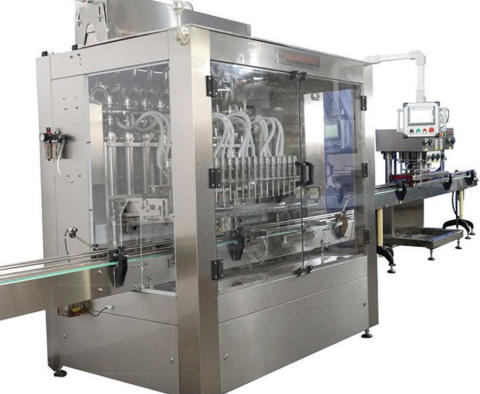
8. Shantou Today Machine Co., Ltd.
Today Machine manufactures diverse packaging machinery covering powders, granules, and liquids. The company emphasizes smart control technologies and export‑friendly standardization. Their liquid packing machines provide precise sealing, anti‑leak mechanisms, and customizable configurations for flow rate and pouch dimensions.
Today Machine exports to more than 60 countries, delivering a balance of affordability and technical sophistication.
9. Ruian Huadong Packing Machinery Co., Ltd.
Ruian Huadong specializes in vertical liquid packaging solutions, particularly suitable for beverages, sauces, and pesticides. Their liquid packing machines utilize microcomputer technology to coordinate filling accuracy with fast sealing operations.
The company's products are popular among small and medium‑sized enterprises thanks to their low maintenance needs and high return on investment. Huadong also offers OEM and ODM services to meet international partners' branding needs.
10. Hangzhou Zhongya Machinery Co., Ltd.
Zhongya Machinery provides automatic filling, capping, and labeling machines for liquid products such as edible oils, detergents, and lubricants. Their designs integrate modern servo systems and fault‑detection technology, ensuring stable production flow.
Zhongya's heavy‑duty construction and user‑friendly HMI interfaces attract large‑scale manufacturing clients looking for durable and customizable machinery from reliable Liquid Packing Machine Manufacturers.
How to Choose the Right Liquid Packing Machine Manufacturer
Selecting the best Liquid Packing Machine Manufacturer depends on production capacity, budget, liquid type, and packaging standards required. Before committing to a supplier, consider these important aspects:
1. Compliance and certification: Ensure the machines meet GMP, CE, or ISO standards, especially for food and pharma industries.
2. Material compatibility: Choose models compatible with liquids of different viscosity or chemical composition.
3. Automation level: Evaluate if semi‑automatic or fully automatic models better fit your operation.
4. After‑sales support: Look for manufacturers providing training, installation, and spare‑part service.
5. Customization needs: Some companies offer turnkey services, like Ningbo Everheal, providing plant planning and production line construction.
Market Outlook for Liquid Packing Machine Manufacturers in China
The Chinese liquid packaging machinery market continues to grow due to rising demand for packaged beverages, pharmaceuticals, and health products. Automation, energy efficiency, and smart control systems are major development trends.
Leading Liquid Packing Machine Manufacturers are investing in IoT‑based monitoring, digital twins, and predictive maintenance to improve uptime and product quality. International buyers increasingly recognize China's capacity to offer both cost‑effectiveness and global‑compliant quality.
From compact tabletop units to high‑capacity automatic filling systems, modern liquid packaging machines are enhancing industries' ability to maintain hygiene, precision, and productivity.
Conclusion
China's Liquid Packing Machine Manufacturers are transforming global packaging standards through innovation, precision, and cost‑efficient engineering. Companies like Ningbo Everheal Medical Equipment Co., LTD. lead this transformation by providing fully customized pharmaceutical production solutions, bridging advanced engineering with international compliance.
Whether you are building a new plant or upgrading an existing production line, choosing a trusted manufacturer ensures dependable performance, consistent product quality, and long‑term value. The top 10 manufacturers listed here represent China's finest expertise in the liquid packaging machinery industry, offering end‑to‑end solutions for every global enterprise.
FAQ
1. What industries use liquid packing machines?
Liquid packing machines are used in pharmaceuticals, food and beverage, cosmetics, and chemical industries to ensure precise filling and contamination‑free sealing of liquid products.
2. What is the difference between automatic and semi‑automatic liquid packing machines?
Automatic machines integrate filling, sealing, and capping in one continuous process, while semi‑automatic machines require manual intervention for one or more steps, offering flexibility for smaller operations.
3. How can I ensure a liquid packing machine meets GMP or FDA standards?
Look for certifications, supplier documentation, and third‑party audits. Reputable firms like Ningbo Everheal design machines according to international pharmaceutical standards.
4. What maintenance do liquid packing machines require?
Routine maintenance includes cleaning filling nozzles, checking seals, verifying calibration, and lubricating mechanical parts to maintain precision and extend machine life.
5. Can these machines handle different viscosity levels?
Yes. Leading Liquid Packing Machine Manufacturers design adjustable systems capable of handling products ranging from watery liquids to thick gels or viscous ointments.


