Content Menu
● What Is a HEPA Air Filter?
● Why Choose Chinese HEPA Air Filter Manufacturers?
● Top 10 HEPA Air Filter Manufacturers in China
>> 1. Everheal Pharmaceutical Equipment Co., Ltd.
>> 2. Camfil Air Filtration (China) Co., Ltd.
>> 3. Shanghai Lingqiao Environmental Protection Equipment Co., Ltd.
>> 4. Suzhou Purification Equipment Co., Ltd.
>> 5. Guangzhou KLC Cleantech Co., Ltd.
>> 6. AAF (American Air Filter) China
>> 7. Zhongshan Zhaohui Filter Co., Ltd.
>> 8. Jiangsu Wintek Environmental Technology Co., Ltd.
>> 9. Beijing Dwin Filtration Equipment Co., Ltd.
>> 10. Shenzhen Yuzheng Purification Technology Co., Ltd.
● Applications of HEPA Air Filters in Industry
● Factors to Consider When Choosing a HEPA Air Filter Manufacturer
● Conclusion
● FAQs
>> 1. What is the efficiency rating of a HEPA air filter?
>> 2. How often should a HEPA filter be replaced?
>> 3. Can Chinese HEPA air filter manufacturers customize products for international clients?
>> 4. Are Chinese HEPA filters compliant with international quality standards?
>> 5. What industries use HEPA air filters the most?
In today's era of industrial automation and pharmaceutical innovation, air purity plays a vital role in ensuring product quality and operational safety. From cleanroom facilities to medical laboratories, HEPA air filters have become an indispensable component. China, known for its robust manufacturing capability and engineering excellence, has evolved into one of the world's leading producers of HEPA filtration systems.
This article introduces the top 10 HEPA air filter manufacturers in China, highlighting their strengths, technological innovations, and market presence. Whether you are sourcing filters for pharmaceutical production, electronic assembly, or healthcare applications, this guide will help you identify reliable suppliers from China's competitive industrial landscape.
What Is a HEPA Air Filter?
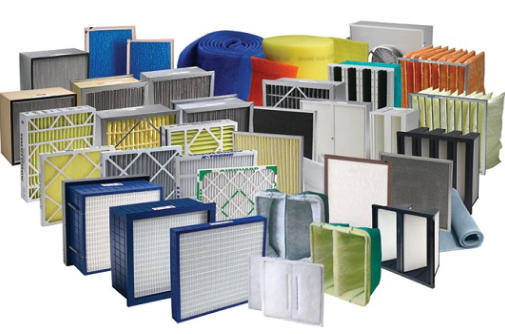
A HEPA (High-Efficiency Particulate Air) filter is designed to capture at least 99.97% of airborne particles measuring 0.3 microns or larger. These filters use a complex web of fibers, typically made from glass or synthetic material, that trap dust, bacteria, and other contaminants.
HEPA filters are widely used in:
- Pharmaceutical manufacturing cleanrooms
- Hospitals and laboratories
- Semiconductor and electronics production lines
- HVAC and air purification systems
- Industrial dust control units
In the pharmaceutical industry, HEPA air filters ensure sterile conditions for drug formulation, filling, and packaging — critical for product safety and compliance with global GMP standards.
Why Choose Chinese HEPA Air Filter Manufacturers?
China's HEPA air filter manufacturers have become key players in the global supply chain due to several competitive advantages:
1. Advanced manufacturing technologies – Chinese suppliers integrate CNC machining, automated filter assembly, and nanofiber production systems.
2. Cost efficiency – Economies of scale and vertically integrated supply chains reduce production costs significantly.
3. Global certifications – Many top companies comply with ISO9001, CE, and GMP quality management standards.
4. Customization capability – Chinese manufacturers offer tailored production for HVAC systems, pharmaceutical laboratories, and cleanroom project needs.
5. International service support – The leading companies provide design, installation, and after-sales support across Asia, Europe, and the Americas.
Let's explore the top names driving this rapidly growing sector.
Top 10 HEPA Air Filter Manufacturers in China
1. Everheal Pharmaceutical Equipment Co., Ltd.
Headquarters: Shanghai, China
Main Products: HEPA air filters, pure steam generators, purified water systems, sterilization units, and cleanroom layouts.
Everheal is a globally recognized innovator specializing in pharmaceutical-grade HEPA air filter systems. The company's filters are engineered for cleanroom environments and meet stringent pharmaceutical production standards. Their expertise extends beyond air purification to complete factory layout planning and production line construction, providing turnkey cleanroom solutions.
With a research-driven team and modern production facilities, Everheal is favored by pharmaceutical companies seeking high-precision filtration integrated with water purification and sterilization technologies.
Core Strengths:
- Comprehensive cleanroom engineering services
- Filters tested for EN1822 and ISO14644 compliance
- Customizable filtration units for GMP facilities
- Strong international service and support network
2. Camfil Air Filtration (China) Co., Ltd.
Headquarters: Kunshan, Jiangsu
Camfil is a global leader with a major production base in China. The company focuses on sustainable and high-efficiency air filtration technologies. Camfil's HEPA filters are widely used in hospitals, biotechnology firms, and electronics manufacturing.
Highlights:
- Premium HEPA and ULPA filter lines
- Research-driven design for low energy consumption
- Long operational lifespan and low pressure drop
- Comprehensive testing and certification
3. Shanghai Lingqiao Environmental Protection Equipment Co., Ltd.
Headquarters: Shanghai
Lingqiao stands out as a trusted supplier of medical and industrial-grade HEPA filters. It produces box-type, separator, and mini-pleat HEPA filters compatible with cleanroom and HVAC systems.
Key Advantages:
- Over 15 years of industry experience
- Automated mini-pleat manufacturing line
- Available in aluminum, galvanized, or stainless steel frames
- High-temperature HEPA models for sterilization rooms
4. Suzhou Purification Equipment Co., Ltd.
Headquarters: Suzhou, Jiangsu
With a strong presence in the Yangtze River Delta, Suzhou Purification specializes in high-efficiency filtration systems for electronics and pharmaceutical facilities. The company's HEPA filters are known for accurate particle retention and exceptional durability.
Features:
- Factory-certified ISO9001 and ISO14001 quality systems
- Custom airflow and resistance configuration options
- Filters designed to integrate seamlessly into HVAC systems
5. Guangzhou KLC Cleantech Co., Ltd.
Headquarters: Guangzhou
KLC Cleantech has become one of the most recognized HEPA air filter manufacturers for cleanroom projects worldwide. Its advanced R&D and automated assembly lines allow the production of both standard and customized HEPA filters.
Core Strengths:
- Wide product range: pre-filters, medium-efficiency filters, HEPA, and ULPA
- Application in pharmaceutical, semiconductor, and healthcare sectors
- Global exports to over 40 countries
- High-efficiency PTFE and glass fiber filter media
6. AAF (American Air Filter) China
Headquarters: Suzhou
AAF, a reputable international brand, has a major manufacturing operation in China. The company delivers advanced synthetic and glass fiber HEPA solutions tailored for critical clean-space control.
Highlights:
- Proprietary media design reducing energy use
- Robust metal frame HEPA filters
- Global quality assurance and international certification
7. Zhongshan Zhaohui Filter Co., Ltd.
Headquarters: Zhongshan, Guangdong
Zhaohui produces a variety of cleanroom filters including HEPA box filters, minipleat filters, and fan filter units (FFUs). The company's filters are used widely in pharmaceutical and microelectronics facilities.
Advantages:
- Competitive pricing with reliable performance
- Multiple frame material options
- Strict particle emission testing in cleanroom facilities
8. Jiangsu Wintek Environmental Technology Co., Ltd.
Headquarters: Yancheng, Jiangsu
Wintek specializes in HEPA and ULPA air filters designed for environmental protection and cleanroom systems. The company offers technical consulting and filtration system engineering in addition to manufacturing.
Strengths:
- Energy-efficient filter materials
- Dust-free workshop production environment
- High efficiency for particles ≥0.3μm
9. Beijing Dwin Filtration Equipment Co., Ltd.
Headquarters: Beijing
Dwin Filtration is an established producer of high-performance HEPA filters for medical and aerospace applications. The company invests heavily in R&D, ensuring advanced quality control technologies at every stage.
Key Strengths:
- Advanced pleating machinery ensuring uniform airflow
- Long service life with stable efficiency
- Customized solutions available for OEM clients
10. Shenzhen Yuzheng Purification Technology Co., Ltd.
Headquarters: Shenzhen
Yuzheng is a modern HEPA filter manufacturer integrating design, production, and global distribution. Its products are widely applied in bioengineering, microelectronics, and pharmaceutical projects.
Features:
- Advanced automated manufacturing lines
- Cleanroom-level inspection and testing procedures
- International shipping and reliable after-sales service
Applications of HEPA Air Filters in Industry
HEPA filters play a decisive role in maintaining contamination-free environments. In pharmaceutical sectors, they are installed in cleanrooms, filling areas, isolators, and HVAC systems, ensuring dust-free sterile operation. For electronics, they prevent particulate interference during microchip assembly.
Key industries using HEPA filters:
- Pharmaceutical production
- Automotive spray booths
- Food and beverage processing
- Optical equipment and lens manufacturing
- Data center HVAC systems
As environmental standards tighten globally, companies increasingly rely on efficient HEPA air filter manufacturers for sustainable and compliant air management systems.
Factors to Consider When Choosing a HEPA Air Filter Manufacturer
Selecting the right manufacturer ensures operational reliability and regulatory compliance. Consider the following aspects:
1. Material quality: Ensure the fiber media and frames meet international safety standards.
2. Efficiency certification: Look for EN1822, ISO 14644, or equivalent certifications.
3. Customization: Evaluate the supplier's ability to design filters for specific production layouts.
4. After-sales service: Availability of maintenance, testing, and installation support.
5. Global experience: Companies with export records often maintain better documentation and process stability.
When these criteria align, you can build a long-term partnership that guarantees cleanroom performance and production quality.
Conclusion
China's HEPA air filter manufacturers have established themselves as global leaders with advanced production capacity, rigorous quality control, and customizable solutions for diverse industries. Companies such as Everheal, Camfil, and KLC Cleantech represent the forefront of China's filtration technology — combining innovation with affordability.
For pharmaceutical and manufacturing clients seeking comprehensive cleanroom and filtration solutions, collaborating with these Chinese manufacturers can ensure both product quality and operational efficiency.
FAQs
1. What is the efficiency rating of a HEPA air filter?
HEPA filters capture at least 99.97% of particles at 0.3 microns, making them suitable for cleanroom and pharmaceutical environments where sterility is essential.
2. How often should a HEPA filter be replaced?
Replacement frequency depends on operational conditions. Typically, filters are changed every 6 to 12 months in cleanroom or laboratory settings.
3. Can Chinese HEPA air filter manufacturers customize products for international clients?
Yes, most top Chinese manufacturers, such as Everheal and KLC Cleantech, provide custom engineering services, design adjustments, and filtration system integration for global buyers.
4. Are Chinese HEPA filters compliant with international quality standards?
Leading producers in China comply with ISO9001, CE, and GMP standards. Many also perform in-house efficiency testing per EN1822 guidelines.
5. What industries use HEPA air filters the most?
They are widely used in pharmaceuticals, biotechnology, microelectronics, aerospace, and medical devices, ensuring clean environments for precision work and sterile production.


